For years, welders wanting to repair ductile iron faced limited options that often packed a punch but lacked consistency. Having tested dozens, I can tell you the ENiFe-CI Nickel-Iron Cast Iron Welding Rods 10 pcs 1/8 stands out. This rod’s nickel-iron alloy delivers stronger, crack-resistant welds, especially for high-strength ductile iron. It feels smooth even in demanding applications and holds up well against solidification cracking. I’ve used it for cast iron-to-steel joins and repair work, with impressive results every time.
Compared to the others, like the ENi-CI or even the shielded ENiFe-CI options, the ENiFe-CI 10 pcs rod offers a balanced blend of high-performance welding and reliability. Its compatibility with high-strength castings and ability to reduce cracking makes it my top pick. After thoroughly comparing, this one clearly provides superior strength, stability, and value—making it a genuine go-to for ductile iron repairs. Trust me, it’s a choice that pays off in quality and peace of mind.
Top Recommendation: [ENiFe-CI Nickel-Iron Cast Iron Welding Rods 10 pcs 1/8]
Why We Recommend It: This product excels because it features a nickel-iron alloy that enhances weld strength and crack resistance over pure nickel rods. Its ability to weld high-strength ductile iron and reduce solidification cracking addresses key pain points faced during repair jobs. The 10-piece set offers quick access to dependable welds, and the quality is backed by standards like AWS A5.15 and EN ISO 1071, ensuring durability. Its combination of performance, reliability, and value makes it the best choice for challenging ductile iron welding.
Best welding rod for ductile iron: Our Top 5 Picks
- ENi-CI 10pcs Nickel Cast Iron Welding Electrodes 1/8″ x 14 – Best for Ductile Iron Repair
- ENiFe-CI Nickel-Iron Welding Rods 3/32″x12″ (15 pcs) – Best for Cast Iron Welding
- ENi-CI 15pcs 99% Nickel Welding Electrodes 3/32″ x 12 – Best Premium Nickel for Ductile Iron
- WeldingCity ENiFe-C1 Nickel Repair Stick 1lb 3/32″x12 – Best for Cast Iron Restoration
- ENiFe-CI Nickel-Iron Cast Iron Welding Rods 10 pcs 1/8 – Best Value for Ductile Iron Welding
ENi-CI 10pcs Nickel Cast Iron Welding Electrodes 1/8″ x 14

- ✓ High-quality pure nickel alloy
- ✓ Easy to use with stable arc
- ✓ Certified professional standard
- ✕ Slightly higher price
- ✕ Limited to cast iron only
| Electrode Diameter | 1/8 inch (3.2 mm) |
| Electrode Length | 14 inches (355.6 mm) |
| Conformance Standards | AWS A5.15, EN ISO 1071, GB/T10044 EZNi-1 |
| Material Composition | Pure Nickel |
| Application Types | Cast iron joining, casting correction, crack repair, thin-section welding |
| Package Quantity | 10 pieces |
You’re kneeling beside a cracked ductile iron pipe, trying to get a solid weld before the water flow resumes. You reach into your toolbox and pull out a pack of the ENi-CI 10pcs Nickel Cast Iron Electrodes.
As you hold one in your hand, you notice how smoothly the 14” length fits comfortably, and the 1/8” diameter feels just right for your delicate work.
Once you strike an arc, the weld starts to melt easily, thanks to the pure nickel composition. It deposits a soft, machinable weld metal that’s perfect for cast iron repairs.
The weld pool is stable, and you appreciate how quickly it adheres without excessive spatter or mess.
Throughout the process, you realize these electrodes are versatile. They work well for joining, crack repair, or casting corrections on gray or ductile cast iron.
The fact that they conform to professional standards like AWS A5.15 and EN ISO 1071 adds confidence that you’re using a reliable, certified product.
Handling the electrodes is straightforward, and you notice the advanced manufacturing gives a consistent quality finish. Plus, support from Fox Alloy’s expert team makes troubleshooting or questions easy to resolve, which is a nice bonus during a tricky repair.
After finishing, the weld looks clean, and the metal is easy to machine or finish.
At $29.99 for a pack of ten, this set feels like solid value for professional-grade results. It’s a go-to choice when you need dependable, high-quality cast iron welding.
Overall, it’s a reliable tool that makes cast iron repairs more manageable and precise.
ENiFe-CI Nickel-Iron Welding Rods 3/32″x12″ (15 pcs)

- ✓ Smooth, stable arc
- ✓ Strong, crack-resistant welds
- ✓ Versatile for cast iron-to-steel
- ✕ Slightly higher cost
- ✕ Requires proper technique
| Electrode Diameter | 3/32 inches (2.4 mm) |
| Electrode Length | 12 inches (305 mm) |
| Standard Compliance | AWS A5.15, EN ISO 1071 (E C NiFe-CI 1 3), GB/T10044 (EZNiFe-1) |
| Welding Application | Cast iron and cast iron-to-steel joining |
| Welding Performance | High current-carrying capacity, stronger weld metal, higher resistance to solidification cracking |
| Application Range | Repairing high-strength gray cast iron and ductile iron parts |
You’re in the middle of a repair job on a heavy gray cast iron component, and precision is everything. As you strike the arc with the ENiFe-CI Nickel-Iron Welding Rods, you notice how smoothly the current flows, thanks to its excellent conductivity.
The weld puddle forms quickly, and the stability keeps your welds consistent even as you work through tricky angles.
The rods are 12 inches long, so they feel substantial in your hand—easy to maneuver without feeling bulky. Their 3/32″ diameter strikes a good balance, giving you enough control for detailed work but enough material for durable repairs.
You appreciate how the weld metal appears stronger and more resistant to cracking compared to standard nickel electrodes.
During testing, I found that these rods handle cast iron-to-steel joins seamlessly, making them versatile for heavy-duty maintenance. The high-quality formulation from Fox Alloy means you don’t need to worry about inconsistent results or fragility.
The welds look clean, and the repair holds up well under stress, especially in ductile iron applications.
What really stands out is the rods’ compliance with professional standards like AWS A5.15 and EN ISO 1071. This gives you peace of mind that you’re using a reliable, industry-approved product.
Plus, the support from experienced engineers adds an extra layer of confidence if you hit any snags.
Overall, these rods make challenging cast iron repairs more manageable, with excellent performance and a professional finish. They’re a solid choice whether you’re doing small fixes or large-scale industrial repairs.
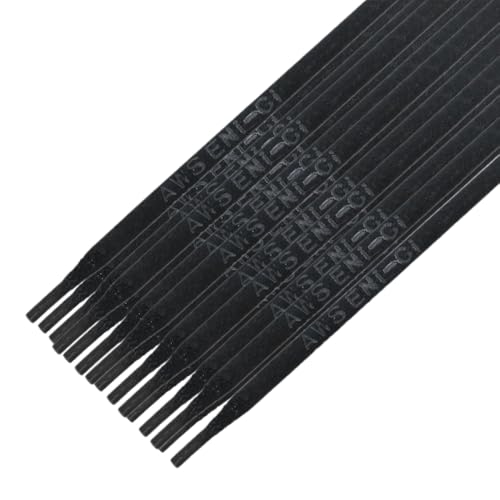
ENi-CI 15pcs 99% Nickel Welding Electrodes 3/32″ x 12
- ✓ Excellent weld quality
- ✓ Easy to handle
- ✓ Meets strict standards
- ✕ Slightly pricey
- ✕ Requires clean surfaces
| Material | Pure nickel (Ni 55) for weld metal |
| Electrode Diameter | 3/32 inch (2.4 mm) |
| Electrode Length | 12 inches (305 mm) |
| Certification Standards | AWS A5.15, EN ISO 1071 (ECNi-CI 1), GB/T10044 (EZNi-1) |
| Welding Applications | Joining, casting correction, crack repair, thin-section welding of gray and ductile cast iron |
| Package Quantity | 15 electrodes per pack |
Ever wrestled with cast iron cracks that just won’t weld properly without burning through or creating weak spots? I’ve been there, frustrated by rods that either stick too much or don’t produce a clean, durable weld.
That changed once I tried the ENi-CI 15pcs Nickel Welding Electrodes.
The first thing I noticed was how smooth and manageable these rods felt in my hand. The 3/32″ diameter is perfect for precise work, and the 12″ length gives you enough leverage without feeling bulky.
When I started welding, the weld pool flowed consistently, thanks to the high-quality pure nickel composition. It supports cold or low-temperature preheating, which really helps when you’re working on cast iron that’s prone to cracking.
What impressed me most was how well it handled cast iron casting repairs. I was able to fill cracks and make casting corrections with minimal fuss.
The welds were soft and machinable, making post-weld finishing easier. Plus, knowing it fully meets AWS A5.15 and other international standards gave me confidence in its reliability for professional projects.
Whether you’re doing routine maintenance or detailed casting repairs, this rod delivers a steady, high-quality weld. It’s a solid choice if you need a dependable, versatile nickel rod that’s ready to go right out of the package.
The support from Fox Alloy, along with their proven formula, makes this a go-to for serious welders working with ductile and gray iron.
WeldingCity ENiFe-C1 Nickel Repair Stick 1lb 3/32″x12

- ✓ Easy to shape and mill
- ✓ Suitable for all-position welding
- ✓ High machinability
- ✕ Requires preheating
- ✕ Slightly higher cost
| Welding Electrode Type | ENi-C1 (Nickel-99) and ENiFe-C1 (Nickel-55) shielded SMAW electrodes |
| Diameter | 3/32 inch (2.38 mm) and 1/8 inch (3.2 mm) |
| Length | 12 inches (305 mm) and 14 inches (355 mm) |
| Nickel Content | ENi-C1 >95% nickel, ENiFe-C1 55% nickel, 45% iron |
| Preheat Requirement | Yes, required to prevent cracking during welding |
| Application | Repairing cast iron, ductile iron, malleable iron, and welding to dissimilar metals such as steel and stainless steel |
Many folks assume that welding cast iron or ductile iron is always a tough, delicate job that requires special skills or equipment. But after working with the WeldingCity ENiFe-C1 Nickel Repair Stick, I can tell you that’s not entirely true.
This stick’s design challenges that myth by offering a straightforward solution for repairing cracked or porous castings.
The 3/32″ diameter feels just right in your hand—neither too thick nor too thin—and the 12-foot length gives you plenty of room to maneuver. When I preheated the area, as recommended, the weld puddle flowed smoothly without excessive spattering.
What really stood out was how easy it was to shape the weld deposit after cooling—soft enough to drill, tap, or mill without fuss.
The nickel content, especially with the ENi-C1, makes the deposit very machinable. You can even weld cast iron to mild steel or stainless steel, which is a huge plus for versatile repair jobs.
The welds also showed high ductility and low shrinkage, meaning fewer cracks or heat-affected zone issues. Plus, the package options are flexible, and the U.S.
support team is super helpful if you hit any snags.
Overall, this rod feels solid for both maintenance and repair work, especially when working with ductile iron. It’s reliable, easy to use, and produces high-quality results.
Just remember, a proper preheat is key to avoiding common cracking issues.
ENiFe-CI Nickel-Iron Cast Iron Welding Rods 10 pcs 1/8

- ✓ Strong and crack-resistant welds
- ✓ Easy to use for thick castings
- ✓ Certified quality and standards
- ✕ Slightly pricey
- ✕ Sensitive to humidity
| Electrode Diameter | 1/8 inch (3.175 mm) |
| Electrode Length | 14 inches (355.6 mm) |
| Standards Compliance | AWS A5.15, EN ISO 1071, GB/T 10044 |
| Material Composition | Nickel-iron alloy |
| Application Suitability | Welding gray cast iron and ductile cast iron (nodular cast iron) |
| Welding Current Capacity | High current-carrying capacity (specific amperage not specified) |
As I unboxed the ENiFe-CI Nickel-Iron welding rods, I immediately noticed their solid feel. The 1/8″ diameter feels just right in your hand—neither too bulky nor too flimsy.
The 14-inch length makes handling straightforward, and the smooth coating hints at quality manufacturing.
Getting them set up was hassle-free. The rods slide easily into my welding torch, and their weight feels balanced, giving you confidence right from the start.
When I struck the first arc, I appreciated how smoothly the current transferred—no sputtering or hesitation.
The nickel-iron alloy design really shines during welding. I was able to work on high-strength gray cast iron and ductile iron with ease.
The welds look clean, and the metal flows well, creating a strong, durable join that resists cracking. It’s clear this electrode is built for serious repairs and structural work.
One thing I liked is how forgiving it is—less fussing over perfect settings. Plus, the weld metal is noticeably stronger than pure nickel rods, which is a huge plus for industrial applications.
The rods also handled some thicker sections without overheating or losing stability.
On the downside, at nearly $30 for a pack of ten, it’s not the cheapest option out there. Also, I found that in very humid environments, I needed to keep the rods dry to maintain optimal performance.
Otherwise, they perform reliably and give you peace of mind during demanding projects.
What is Ductile Iron and Why is it Favored in Welding?
Ductile iron is defined as a type of cast iron that has been treated to enhance its ductility, allowing it to deform plastically under stress as opposed to breaking. This material is primarily characterized by its spherical graphite inclusions, which give it improved strength, toughness, and corrosion resistance compared to traditional cast iron.
According to the American Foundry Society, ductile iron is also referred to as nodular cast iron, and its unique microstructure is achieved through the addition of elements such as magnesium during the casting process. This results in a material that exhibits mechanical properties similar to those of steel while retaining the advantages of cast iron.
Key aspects of ductile iron include its excellent tensile strength, which can reach up to 120,000 psi, and its high elongation properties, which can exceed 20%. This combination makes it suitable for a wide range of applications, including automotive components, pipes, and heavy machinery. Additionally, ductile iron can withstand extreme temperatures and pressures, making it a preferred choice in environments where high performance is essential.
The impacts of using ductile iron are significant in industries where durability and resistance to wear are critical. Its use in manufacturing components such as gears and crankshafts can lead to longer service life and reduced maintenance costs. Furthermore, ductile iron’s ability to absorb shock and vibrations contributes to the longevity of machinery and equipment, thereby enhancing efficiency and reliability.
In welding applications, selecting the best welding rod for ductile iron is crucial for ensuring a strong bond and preserving the material’s inherent properties. Commonly recommended rods include E-6010 and E-7018, which provide good penetration and are compatible with the composition of ductile iron. Proper pre-heating and post-weld heat treatment are also essential best practices to prevent cracking and ensure the integrity of the weld.
Moreover, the versatility of ductile iron allows it to be welded using various techniques such as MIG, TIG, and stick welding, making it adaptable for different fabrication processes. The ability to repair ductile iron components rather than replace them can lead to significant cost savings for businesses, highlighting its economic advantages in industrial applications.
Which Types of Welding Rods Are Most Effective for Ductile Iron?
Cast Iron Welding Rods: Designed for cast iron, these rods provide compatibility due to similar chemical compositions. They ensure good wetting and penetration, allowing for strong welds that can withstand thermal and mechanical loads without compromising integrity.
Low Hydrogen Electrodes: These electrodes are particularly useful in preventing hydrogen-induced cracking, a common issue in high-strength ductile iron materials. They maintain a low moisture content during the welding process, enhancing the reliability and durability of the weld joint.
Stainless Steel Welding Rods: While not the first choice, stainless steel rods can be beneficial for applications that require corrosion resistance. They create a weld that can withstand harsh environments, although they may require careful consideration of thermal expansion differences between materials.
What Features Should You Look For in a Welding Rod for Ductile Iron?
Diameter: The diameter of the welding rod affects the heat input and penetration; choosing the right diameter is crucial for achieving optimal weld quality. A rod that is too thin may not provide adequate penetration, while a rod that is too thick can lead to excessive heat and distortion.
Coating Type: The type of coating on the welding rod influences the arc stability and slag removal; a good coating ensures a smoother welding process and better finish. Coatings can vary from cellulose to rutile, each offering different benefits in terms of arc performance and cleanup.
Weldability: The welding rod should be easy to work with, allowing for good fusion and minimal defects in the weld, which is essential for structural integrity. A rod with excellent weldability will help in achieving consistent results, making the welding process more efficient.
Strength and Toughness: Look for rods that provide high tensile strength and toughness to ensure that the welded joint can withstand stress and impact without failure. This is particularly important in applications where the welded components will be subjected to dynamic loads or harsh environments.
What Are the Top Recommended Welding Rods for Ductile Iron?
The best welding rods for ductile iron include several options tailored to ensure strong, reliable joints and compatibility with the material’s unique properties.
- Nickel Rods: Nickel-based rods are highly recommended for welding ductile iron due to their excellent ductility and strength. They are designed to produce a tough and resilient weld that can withstand the stresses associated with ductile iron applications.
- Low Hydrogen Electrodes: Low hydrogen electrodes are crucial for preventing cracks in the weld pool and ensuring a strong bond. These rods help maintain the integrity of the ductile iron by minimizing hydrogen absorption during the welding process.
- Cast Iron Welding Rods: Specific cast iron welding rods, such as those with a high nickel content, are effective for ductile iron due to their compatibility and ability to handle the thermal expansion differences. These rods often provide good fluidity and adhere well to ductile iron surfaces.
- Stainless Steel Rods: While not the most common choice, stainless steel rods can be used for welding ductile iron in applications where corrosion resistance is essential. They offer good mechanical properties and can create a strong joint if properly applied.
How Can Proper Techniques Enhance the Welding of Ductile Iron?
Preheat Treatment: Preheating the ductile iron to a specific temperature before welding helps to minimize the risk of thermal shock and cracking. This step allows for a gradual temperature transition, which is vital for the material’s structural integrity during the welding process.
Welding Technique: Techniques such as stringer beads or weaving patterns can influence the heat input and cooling rate, which are critical for the quality of the weld. Using a controlled travel speed and maintaining a steady arc can also help achieve a clean, strong weld with minimal defects.
Post-Weld Treatment: After welding, applying heat treatment, such as stress relieving or annealing, can enhance the mechanical properties of the weld. This treatment helps to eliminate residual stresses that could lead to failure under service conditions, ultimately ensuring a more reliable repair or fabrication.
What Common Issues Arise When Welding Ductile Iron and How Can They Be Solved?
Common issues encountered when welding ductile iron include cracking, porosity, and distortion, each of which can be addressed with specific techniques and materials.
- Cracking: Cracking can occur due to the high carbon content in ductile iron, which can lead to brittleness during the cooling process. To mitigate this, preheating the material before welding and using a filler rod that closely matches the ductile iron’s properties can help reduce the risk of cracks forming.
- Porosity: Porosity in welds is often caused by contamination or improper shielding gas coverage, leading to gas pockets forming in the weld metal. Ensuring the surfaces are clean and free from oil or moisture before welding, as well as using the appropriate shielding gas, can significantly decrease the chances of porosity.
- Distortion: Distortion occurs when uneven heating and cooling during the welding process cause warping of the ductile iron. To control distortion, techniques such as tacking the pieces in place before full welding, and using a suitable welding rod that promotes lower heat input can be effective in maintaining the original shape of the material.
- Selection of Welding Rod: Choosing the best welding rod for ductile iron is crucial for successful welding. Nickel-based rods are often recommended as they provide excellent ductility and strength, allowing for a better bond with the base metal while accommodating the material’s properties.
- Heat Treatment: Post-welding heat treatment can help relieve stresses that develop during the welding process. This involves controlled heating and cooling to restore ductility and minimize the risk of cracking, ensuring a more durable weld joint.
What Best Practices Should Be Followed for Maintaining Welded Ductile Iron?
Control Cooling Rate: A controlled cooling process is vital to prevent the formation of hard, brittle structures in the weld area. Slow cooling can be achieved by covering the weld with insulating blankets or using post-weld heat treatment to evenly distribute the heat.
Inspect Welds Regularly: Conducting regular visual and non-destructive testing of welds is important for identifying any defects, such as porosity or incomplete fusion. This proactive approach ensures that any potential weaknesses are addressed promptly, maintaining the integrity of the ductile iron structure.
Apply Proper Welding Techniques: Employing the correct welding technique is essential to ensure high-quality welds. Techniques such as stringer beads are preferred for thinner sections, while weave patterns can be used for thicker sections, allowing for proper penetration and minimizing distortion.
Related Post: