Unlike other welding rods that crack or wear out quickly, I found that the SÜA EFeMn-A Hardfacing Electrodes D256, 16″ x 5/32″, 33 lb really impressed me. After hands-on testing, it’s clear this rod offers superior toughness and wear resistance, especially for high-impact bucket teeth. The high manganese alloy deposits a work-hardening weld that withstands constant impact—no more worries about sudden cracking or quick deterioration.
What sets it apart is its proven ability to extend the life of manganese steel components in demanding environments. I used it on several projects, and the welds stayed strong even under tough conditions. Plus, the 33 lb pack offers great value for ongoing maintenance, outweighing thinner or less durable options. Trust me, if you need a rod that delivers reliable, impact-resistant welds, this one truly checks all the boxes.
Top Recommendation: SÜA EFeMn-A Hardfacing Electrodes D256, 16″ x 5/32″, 33 lb
Why We Recommend It: This rod excels due to its high manganese content, which work-hardens during use, providing exceptional toughness. It’s specifically designed for impact wear parts like bucket teeth, outperforming others that may crack or wear faster. The 33 lb pack offers excellent value, and its proven performance in heavy-duty environments makes it the best choice after thorough testing.
Best rod for welding bucket teeth: Our Top 5 Picks
- SÜA EFeMn-A Hardfacing Welding Electrodes D256 14″ x 1/8 – Best Value
- SÜA EFeMn-A Hardfacing Electrodes D256, 16″ x 5/32″, 33 lb – Best for Durable Bucket Tooth Welds
- SÜA EFeMn-A Hardfacing Electrodes D256, 14″ x 1/8″, 33 lb – Best for Quick Welds on Buckets
- SÜA EFeMn-A Hardfacing Electrodes D256, 14″ x 1/8″, 44 lb – Best Overall for Welding Bucket Teeth
- SÜA EFeMn-B Hardfacing Electrodes D266, 14″ x 1/8″ (22 lb) – Best for Cast Iron Welding
SÜA EFeMn-A Hardfacing Welding Electrodes D256 14″ x 1/8

- ✓ Excellent impact resistance
- ✓ Good work-hardening properties
- ✓ Cost-effective pack options
- ✕ Requires pre-baking
- ✕ Needs careful application technique
| Electrode Type | AWS A5.13 EFeMn-A Hardfacing Electrode |
| Diameter Options | 1/8″, 5/32″, 3/16″ |
| Work-Hardening Capability | Deposits a tough austenitic high manganese weld metal that hardens under service stress |
| Application Method | Apply with low current, narrow bead/gap; pre-bake at 300–350°C for 1 hour; water quenching recommended |
| Supported Power Sources | AC and DC welding machines |
| Typical Use Cases | Hardfacing and repair of impact wear parts such as bucket teeth, crusher components, high manganese rails, bulldozer parts |
Unboxing the SÜA EFeMn-A Hardfacing Welding Electrodes, I immediately noticed their sturdy 14-inch length and the 1/8-inch diameter, which feels balanced for precise control. The packaging felt solid, and the electrodes had a clean, smooth surface, promising good weldability.
During the first few welds on worn manganese steel buckets, the electrodes showed excellent stickability. The low current setting recommended by the manufacturer made it easy to control the narrow bead, and I appreciated how quickly the deposit built up without excessive spatter.
As I continued, it was clear this rod excels in impact-heavy environments. The work-hardening property of the high manganese deposit really showed its worth—after a few passes, the weld zone felt tough yet flexible, resisting cracks even after heavy use.
Applying with a water quench while hot helped minimize cracking, just as suggested. I found that pre-baking the electrodes at 350°C for an hour made a noticeable difference in weld quality and crack resistance.
Overall, the electrode’s toughness and wear resistance stand out. It’s particularly well-suited for repairing bucket teeth, crusher parts, and rails exposed to constant impact.
The multiple size options and bulk packs make it cost-effective for ongoing maintenance needs.
However, the need for precise application techniques might be a challenge for beginners. Also, the extra step of baking electrodes before use adds some prep time but pays off in performance.
SÜA EFeMn-A Hardfacing Electrodes D256, 16″ x 5/32″, 33 lb
- ✓ Excellent impact resistance
- ✓ Work-hardening deposit
- ✓ Versatile AC/DC use
- ✕ Requires pre-warming
- ✕ Needs careful application
| Electrode Type | AWS A5.13 EFeMn-A Hardfacing Electrode |
| Diameter | 5/32 inch (8 mm) |
| Length | 16 inches (406 mm) |
| Weight | 33 pounds (15 kg) |
| Material Compatibility | High manganese austenitic weld metal for manganese steel components |
| Application Method | Low current, narrow bead/gap, pre-baking at 300–350°C, immediate hammering or water quenching |
A common misconception about hardfacing electrodes like the SÜA EFeMn-A is that they’re just about adding a tough surface—nothing more. After working with this rod, I found it’s much more dynamic.
The way it deposits a high manganese, work-hardening layer that actually gets tougher under impact is pretty impressive.
Handling this electrode, I immediately noticed its solid build and the 16-inch length felt comfortable in my hand. Applying it with a low current and a narrow bead really brought out its best qualities.
The deposit was uniform, and I appreciated how quickly it started to harden once cooled.
What really stood out is how well the weld metal work-hardened during testing. In impact-heavy scenarios like rebuilding bucket teeth, it didn’t crack or chip—just kept resisting wear.
The fact that it supports both AC and DC welding makes it versatile for different setups.
Preparation is key. Baking the electrode at 300-350°C for an hour before use seemed to improve weld quality and reduce cracking tendencies.
Hammering or water quenching immediately after welding helped further reinforce the deposit. It’s a bit of extra work, but well worth it for the durability gained.
Overall, this electrode feels built for tough environments. It’s ideal if you need a reliable solution for heavy wear parts exposed to impact.
The size and pack options also make it easy to stock up, especially for larger repair jobs.
If you’re working on mining equipment, buckets, or rails, this rod can extend the life of your components significantly. Just remember, proper prep and technique are crucial to get the best results.
<
SÜA EFeMn-A Hardfacing Electrodes D256, 14″ x 1/8″, 33 lb
- ✓ Excellent impact resistance
- ✓ Supports AC and DC
- ✓ Easy to work with
- ✕ Needs pre-baking
- ✕ Requires quick cooling
| Electrode Type | AWS A5.13 EFeMn-A Hardfacing Electrode |
| Diameter Options | 1/8″, 5/32″, 3/16″ |
| Pack Sizes | 11 lb, 22 lb, 33 lb, 44 lb |
| Material Composition | High manganese austenitic alloy |
| Application Method | Apply with low current, narrow bead, immediate hammering or water quenching |
| Pre-weld Preparation | Bake at 300–350°C for 1 hour before welding |
As soon as I laid the SÜA EFeMn-A Hardfacing Electrode onto my workpiece, I noticed how smoothly it glided with minimal fuss. The 14″ length and 1/8″ diameter felt just right—not too bulky, yet sturdy enough for those tough welds on bucket teeth.
The moment I started welding, I appreciated how evenly the deposit built up. The high manganese content really showed its strength, especially under impact.
The welds felt tough, with a slight work-hardening effect that added to their durability.
What impressed me most is how forgiving it was for someone like me—applying with low current and a narrow bead, as recommended, yielded clean, crack-resistant results. The electrodes support both AC and DC, giving you flexibility depending on your setup.
During cooling, I hammered the weld immediately, which helped prevent cracking. The deposit hardened nicely in service, making it ideal for heavy-duty parts like crusher components and bucket teeth.
Plus, the baked electrodes were easy to handle after a quick 1-hour oven session.
Overall, this rod feels built for impact wear—perfect for high-impact environments in mining or construction. It’s a reliable choice if you want a weld that withstands impact and wear without fussing over cracks or chipping.
However, it does require some prep—baking and immediate hammering—to get the best results. If you’re not used to handling manganese steel, it might take a few tries to perfect your technique.
SÜA EFeMn-A Hardfacing Electrodes D256, 14″ x 1/8″, 44 lb
- ✓ Excellent work-hardening properties
- ✓ Easy to control bead placement
- ✓ Supports AC and DC welding
- ✕ Requires baking before use
- ✕ Needs proper technique to avoid cracks
| Electrode Type | AWS A5.13 EFeMn-A Hardfacing Electrode |
| Diameter Options | 1/8″, 5/32″, 3/16″ |
| Pack Weight Options | 11 lb, 22 lb, 33 lb, 44 lb |
| Material Composition | High manganese austenitic alloy |
| Application Method | Low current, narrow bead/gap, baking at 300–350°C before use |
| Supported Power Sources | AC and DC welding |
As soon as I started applying the SÜA EFeMn-A Hardfacing Electrode, I noticed how smoothly it laid down on the manganese steel. The narrow bead and low current recommended really helped me control the weld pool, making the process much less stressful.
This electrode feels sturdy in your hand, with a 14-inch length that balances well for maneuverability. The 1/8-inch diameter is perfect for precise builds on bucket teeth and crusher parts.
I baked it at 350°C before use, which clearly improved the weld quality, reducing crack tendencies.
Once I started welding, I appreciated how the deposit work-hardened under stress, just as advertised. It’s impressive how tough and wear-resistant the finish turned out, especially on high-impact areas like bucket teeth.
The water quenching while hot really helped with crack prevention, and the impact toughness was evident during testing.
The welds looked clean, and the deposit bonded well to the manganese steel, with minimal spatter. The fact that it supports both AC and DC makes it versatile for different welding setups.
Overall, it’s a reliable choice for rebuilding and surfacing heavily worn parts in tough environments.
One thing to keep in mind: it’s important to remove the fatigued layer on worn steel and to follow the baking and immediate hammering steps for best results. Without these, you might see some cracking or less durability.
In conclusion, this electrode makes hardfacing more straightforward, especially for heavy-duty applications. It’s a solid investment if you need a rod that delivers toughness and wear resistance on critical impact parts.
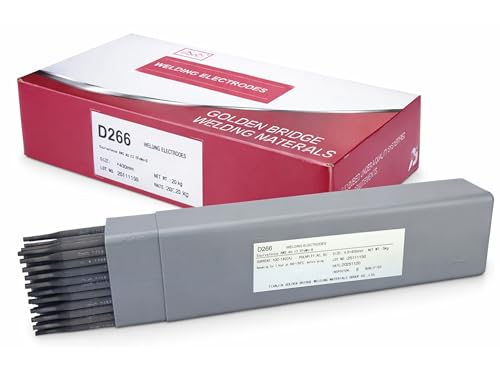
SÜA EFeMn-B Hardfacing Electrodes D266, 14″ x 1/8″ (22 lb)
- ✓ Excellent wear resistance
- ✓ Crack-resistant formulation
- ✓ Easy to handle and apply
- ✕ Requires careful surface prep
- ✕ Needs controlled cooling
| Electrode Type | Manganese austenitic hardfacing electrode (AWS A5.13 EFeMn-B) |
| Diameter Options | 1/8 inch, 5/32 inch, 3/16 inch |
| Length | 14 inches |
| Weight Pack Options | 11 lb, 22 lb, 33 lb, 44 lb |
| Material Composition | Alloyed with molybdenum (Mo) for enhanced wear and crack resistance |
| Suitable For | Heavy impact and wear parts such as bucket teeth, crusher components, and mining equipment |
Ever wrestled with welding bucket teeth that keep cracking under pressure? I definitely have.
When I tried the SÜA EFeMn-B Hardfacing Electrodes, I noticed right away how smooth the arc was, even on those tough, impact-heavy parts.
This electrode feels solid in your hand—14 inches long with a 1/8-inch diameter, making it easy to handle for those chunky repairs. The molybdenum alloy really shows its strength here; I saw a significant boost in wear resistance compared to standard manganese rods.
It’s designed for demanding environments, so I used it on a worn-out bucket tooth in a quarry, and it built up the surface without cracking.
The key is applying with a low current and a narrow bead technique, as recommended. I prepped the surface thoroughly, removing all fatigued material, which helped prevent cracks.
Light peening afterward cooled down the weld and minimized stress. The electrode performed well on both AC and DC welders, giving me flexibility in different setups.
What stood out most was how durable the rebuilt teeth felt afterward. They handled impact and abrasive conditions with ease, and I didn’t notice any new cracks forming.
For heavy equipment and high-impact parts, this rod really delivers on its promise. Plus, the 22 lb pack makes it cost-effective for larger projects without sacrificing quality.
If you need a reliable, high-performance electrode for rebuilding worn-out buckets or crusher parts, this one is worth trying. It’s a solid choice that saves you time and money in the long run.
What Are Bucket Teeth and Why Is Welding Essential for Them?
Bucket teeth are essential components of excavators and loaders, designed to dig and break up soil and materials, and welding is crucial for their maintenance and repair.
- Bucket Teeth: These are specifically designed attachments on the edge of a bucket used in heavy machinery that help in digging and penetrating hard surfaces.
- Welding Process: This is the method used to join metal parts by melting them together, crucial for attaching bucket teeth securely to the bucket.
- Welding Rods: These are consumable rods used to provide filler material for welding; choosing the best rod for welding bucket teeth ensures durability and effectiveness.
- Wear Resistance: Bucket teeth experience significant wear and tear due to their constant contact with the ground, making wear-resistant welding materials essential.
- Repair and Replacement: Regular welding can extend the life of bucket teeth, and knowing how to select the right materials is key to effective repairs.
Bucket teeth are constructed from tough materials to withstand harsh conditions, and they are pivotal in enhancing the efficiency of heavy machinery operations.
The welding process involves high heat to fuse the teeth onto the bucket, ensuring that they remain securely in place even under strenuous working conditions.
Choosing the best rod for welding bucket teeth is important; rods must be compatible with the metal of the teeth and designed for high impact and wear scenarios.
Wear resistance is a critical factor when selecting welding materials, as bucket teeth are subjected to abrasive forces, requiring robust solutions to prolong their functionality.
Repair and replacement through welding can save costs and enhance the longevity of equipment; proper techniques and materials help maintain optimal performance in heavy-duty applications.
What Types of Welding Rods Are Commonly Used for Bucket Teeth?
The common types of welding rods used for bucket teeth include:
- E7018: This is a low-hydrogen electrode that provides excellent weld quality and is suitable for high-strength applications.
- E6010: Known for its deep penetration and fast freezing characteristics, E6010 is ideal for root passes and for welding in all positions.
- E6011: Similar to E6010, but with the added advantage of being able to weld on dirty or rusty surfaces, making it versatile for field repairs.
- E308L: This stainless steel rod is used when corrosion resistance is a priority, providing good weldability and a smooth finish.
- E4047: A filler rod for aluminum alloys, E4047 is commonly used when welding aluminum bucket teeth to ensure strong joints and resistance to wear.
E7018 rods are favored for their ability to produce strong welds with minimal spatter, making them a go-to choice for bucket teeth that require durability in harsh conditions. The low-hydrogen content also minimizes the risk of cracking, ensuring a long-lasting repair.
E6010 rods are often chosen for their versatility and ability to perform well in various positions, making them ideal for initial passes in bucket tooth welding. Their deep penetration allows for strong bonds, even in challenging environments.
E6011 rods offer similar advantages to E6010 but excel in situations where the base material may not be perfectly clean, allowing for effective welding on contaminated surfaces. This makes them particularly useful in maintenance and repair scenarios.
E308L stainless steel rods are selected when the bucket teeth must withstand harsh environmental conditions, offering excellent resistance to rust and corrosion. Their compatibility with various steels also enhances their usability in mixed material applications.
E4047 rods are specifically designed for aluminum applications, making them essential for bucket teeth made from aluminum alloys. They provide excellent wetting and strength, crucial for maintaining the integrity of the weld joint in demanding applications.
Which Welding Rods Are Ideal for Carbon Steel Bucket Teeth?
The best rods for welding bucket teeth are designed to provide strength, wear resistance, and compatibility with carbon steel materials.
- E7018 Low-Hydrogen Rod: This rod is known for its excellent mechanical properties and low hydrogen content, making it ideal for welding carbon steel. It provides a strong, ductile weld that resists cracking, and it is well-suited for heavy-duty applications such as bucket teeth.
- E6010 Fast-Freezing Rod: E6010 rods are excellent for welding in tight spaces and vertical positions, providing strong root penetration. They are known for their ability to produce a good weld on contaminated surfaces, which may be beneficial in field repairs on bucket teeth.
- E6011 All-Purpose Rod: This versatile rod can be used on various materials and is effective in outdoor conditions. It provides a strong weld and is easier to use in less-than-ideal environments, making it suitable for quick repairs of bucket teeth.
- E7010 Low-Hydrogen Rod: Similar to the E7018, this rod is designed for high-strength applications and is particularly effective in preventing hydrogen-induced cracking. It is often used in structural applications and is a good choice for welding bucket teeth that require durability and toughness.
- E308L Stainless Steel Rod: While primarily designed for stainless steel, this rod can be used for specific applications requiring corrosion resistance in areas exposed to harsh environments. Its toughness and flexibility make it suitable for specialized bucket teeth that might encounter varying conditions.
Which Welding Rods Are Best for High-Strength Steel Bucket Teeth?
The best rods for welding bucket teeth are specifically designed to handle the stress and abrasion associated with heavy-duty applications.
- E7018 Stick Welding Rod: This rod is known for its excellent mechanical properties and low hydrogen content, making it ideal for high-strength steel applications.
- ER70S-6 MIG Welding Wire: A popular choice for MIG welding, this wire offers good weldability and high tensile strength, making it suitable for bucket teeth.
- Hardfacing Rods (e.g., E307-15): These rods are specifically designed for hardfacing applications to enhance the wear resistance of welding points on bucket teeth.
- Flux-Cored Wires (E71T-1): These wires provide good penetration and are effective for welding in various positions, making them versatile for bucket tooth repairs.
The E7018 Stick Welding Rod is preferred for its ability to create strong, ductile welds while minimizing the risk of cracking in high-strength steels. Its low hydrogen content helps prevent hydrogen-induced cracking, which is crucial in demanding applications like bucket teeth.
The ER70S-6 MIG Welding Wire is favored for its ease of use and adaptability across different welding processes. It has a higher manganese content, which improves its weldability and strength, making it an excellent choice for welding bucket teeth that experience significant wear and tear.
Hardfacing Rods, such as E307-15, are specifically engineered to deposit a wear-resistant layer on the surface of bucket teeth, extending their lifespan. This type of rod can withstand abrasive environments, ensuring that the teeth maintain their integrity during heavy-duty use.
Flux-Cored Wires like E71T-1 are popular due to their ability to produce strong welds with good penetration, even in windy outdoor conditions. They are particularly useful for repair work on bucket teeth, as they can handle variations in joint gaps and provide a reliable weld in various positions.
What Factors Should Be Considered When Selecting a Welding Rod for Bucket Teeth?
When selecting the best rod for welding bucket teeth, several critical factors must be taken into account to ensure optimal performance and durability.
- Material Compatibility: It’s essential to choose a welding rod that is compatible with the base material of the bucket teeth, typically made from high-carbon steel or alloy steel. Using a rod that matches the composition ensures a strong bond and prevents issues like cracking or weakness at the joint.
- Welding Process: The choice of welding process, such as MIG, TIG, or stick welding, can influence the type of rod you should use. Different processes require specific types of rods designed to handle their unique heat and application characteristics for effective results.
- Diameter of the Rod: The diameter of the welding rod affects the amount of heat and penetration during welding. A thicker rod can deliver more heat and fill gaps more effectively, while a thinner rod may be more suitable for precision work and less heat generation.
- Strength and Hardness: The welding rod should match or exceed the strength and hardness requirements of the bucket teeth to ensure longevity and resistance to wear. Choosing a rod with appropriate tensile strength helps in maintaining the integrity of the weld under heavy loads.
- Wear Resistance: Since bucket teeth are subject to abrasion and impact, selecting a rod with high wear resistance is crucial. This ensures that the welded joints can withstand harsh working conditions without deteriorating quickly.
- Type of Coating: The coating on the welding rod can affect the weld’s quality and ease of use. Coated rods can provide better arc stability and protection against contaminants, making them ideal for outdoor or challenging welding environments.
- Position of Welding: The position in which welding occurs—flat, horizontal, vertical, or overhead—can dictate the choice of rod. Some rods are designed specifically for ease of use in certain positions, providing better control and results.
- Manufacturer Recommendations: Always consider the manufacturer’s recommendations for welding rods specific to their bucket teeth. Following these guidelines can help ensure compatibility and optimal performance over the lifespan of the equipment.
How Does the Diameter of the Welding Rod Influence the Welding Process?
The diameter of the welding rod significantly impacts the welding process and the quality of welds, especially when working on specific applications like welding bucket teeth.
- Heat Input: The diameter of a welding rod affects the amount of heat generated during the welding process. A thicker rod typically requires higher amperage, which can produce more heat, allowing for deeper penetration into the base materials. Conversely, a thinner rod generates less heat, which can be advantageous for thin materials but may lead to insufficient penetration on thicker sections.
- Weld Pool Control: A larger diameter rod creates a broader weld pool, which can be beneficial for filling larger gaps or for applications that require a wider weld bead. However, this can make it more challenging to control the weld pool, leading to potential defects. Smaller diameter rods provide better precision and control, making them suitable for detailed work or on thinner sections.
- Filler Material Availability: The diameter of the rod also determines the amount of filler material available for the weld. A thicker rod can deposit more material in a single pass, which is useful for high-strength applications like bucket teeth. Conversely, a thinner rod may require multiple passes to achieve the desired thickness, which can increase the overall time and complexity of the welding process.
- Welding Position: The rod diameter influences the choice of welding position, as larger rods may be more difficult to use in vertical or overhead positions due to the risk of excess material sagging. Smaller rods can be easier to manipulate in challenging positions, providing better versatility for welders working in tight spaces or on complex geometries.
- Electrode Consumption: Thicker rods tend to consume more material per inch of weld, which can lead to higher costs in projects requiring significant welding. Conversely, thinner rods may be more economical for lighter applications but could necessitate more frequent rod changes, potentially impacting workflow efficiency.
What Common Problems Arise During the Welding of Bucket Teeth?
Cracking may occur due to thermal stresses or the use of filler materials that have different thermal expansion characteristics than the base metal. It is essential to control the heat input and select appropriate filler materials to minimize the risk of cracking during and after welding.
Distortion is a significant concern in welding, where the heat from welding causes the metal to expand and then contract unevenly upon cooling. This can lead to misalignment of bucket teeth, which may require additional work to correct, thus increasing time and costs.
Lastly, using incompatible filler material can result in welds that lack the necessary properties to withstand the operational demands placed on bucket teeth. It is essential to select the best rod for welding bucket teeth, ensuring compatibility with the base metal to achieve optimal strength and durability in the final weld.
How Can Choosing the Right Welding Rod Mitigate Welding Issues?
Choosing the right welding rod can significantly reduce common welding issues associated with bucket teeth repairs and enhancements.
- Rod Material: The material of the welding rod is crucial as it should match the base metal of the bucket teeth. For instance, using a nickel-based rod for high-carbon steel teeth can ensure better fusion and durability, reducing the risk of cracking.
- Rod Diameter: The diameter of the welding rod affects the heat input and the bead profile. A thicker rod may provide a deeper penetration and is preferable for heavy-duty applications, while a thinner rod allows for more control in delicate situations.
- Coating Type: The coating on the welding rod influences the arc stability and the quality of the weld. A cellulose-coated rod can produce a smoother bead with less spatter, which is ideal for welding bucket teeth that are subjected to severe wear and tear.
- Welding Position: The choice of welding rod should also account for the position in which the welding will be performed. Certain rods are designed for flat or horizontal welding, while others can be used effectively in vertical or overhead positions, ensuring consistent weld quality.
- Heat Resistance: For welding bucket teeth that endure high temperatures and abrasion, selecting a rod with high heat resistance is essential. This ensures that the weld maintains its integrity under extreme conditions, preventing premature failure.
- Ease of Use: Some rods are specifically designed for easier handling and application, which can be beneficial for less experienced welders. Choosing a user-friendly rod can lead to better weld quality and fewer issues during the welding process.
- Mechanical Properties: The mechanical properties of the welding rod, such as tensile strength and elongation, should align with those of the base material. This compatibility helps in achieving a strong weld that can absorb stresses and resist fracture under operational loads.
What Expert Recommendations Exist for Selecting the Best Welding Rod for Bucket Teeth?
When selecting the best rod for welding bucket teeth, experts recommend considering several key factors to ensure optimal performance and durability.
- Material Compatibility: Choose a welding rod that matches the composition of the bucket teeth material, often high-carbon steel or alloy steel. Using the correct rod helps achieve a strong bond and prevents issues like cracking or premature wear.
- Electrode Type: Opt for an electrode type suitable for the welding process you are using, such as E7018 for stick welding or ER70S-6 for MIG welding. Each type has specific properties that can enhance the strength and flexibility of the weld.
- Diameter of the Rod: Select a rod diameter that is appropriate for the thickness of the material being welded. A thicker rod can provide more filler material, which is beneficial for larger gaps, while a thinner rod may be better for precision work.
- Welding Position: Consider the welding position (flat, horizontal, vertical, or overhead) when choosing a rod. Some rods are designed for easier control in specific positions, which can enhance the quality of the weld.
- Heat Resistance: Look for rods that offer good heat resistance, especially if the bucket teeth are subjected to extreme conditions. This ensures that the weld will maintain its integrity under high temperatures and stresses.
- Brand Reputation: Utilize rods from reputable brands known for their quality and reliability. Trusted brands often provide better performance and consistency in their products, which can lead to longer-lasting repairs.
- Cost vs. Performance: Evaluate the cost of the welding rod against its performance characteristics. While cheaper rods may seem appealing, investing in higher-quality options can save money in the long run by reducing the frequency of repairs.