The first thing that struck me about the SONNLER ER4043 3/32″x 16″ 1.8LB Aluminum TIG Welding Wire Filler Rod wasn’t its size but its remarkably stable arc and minimal spatter when I tested it on different aluminum alloys. It’s smooth to feed, melts evenly, and helps produce crisp, clean welds—perfectly tackling common issues like cracking and uneven flow that often trip up hobbyists and pros alike.
After comparing it closely with other options, this rod’s key advantage is its consistent performance across a broad range of alloys and thicknesses. While the Cadhena 5356 offers great corrosion resistance and MorningRo ER5356 boasts larger capacity for heavy-duty work, SONNLER’s ER4043 outshines by providing a stable, low-spatter weld in even tricky conditions. I highly recommend it for anyone serious about high-quality aluminum TIG welding—you won’t be disappointed.
Top Recommendation: SONNLER ER4043 3/32″x 16″ 1.8LB Aluminum TIG Welding Wire Filler Rod
Why We Recommend It: This product stands out due to its excellent arc stability and minimal spatter, which are critical for clean, professional welds. Its 5% silicon content improves melt pool liquidity, making it easier to weld with precision across a variety of aluminum alloys like 3003, 6061, and 5052. Compared to larger capacity or different alloy-specific rods, it delivers consistent quality for both small repairs and detailed projects, making it the best overall choice after thorough testing.
Best filler rod for tig welding aluminum: Our Top 5 Picks
- ER4043 3/32″x 16″ 1.8LB Aluminum TIG Welding Wire Filler Rod – Best for General Aluminum TIG Welding
- ER4043 1/16″x 16″ 1.8LB Aluminum TIG Welding Wire Filler Rod – Best for Precise Thin-Wall Aluminum Welding
- Cadhena 5356 Aluminum Tig Filler Rods, 25 pcs, 1/16″ x 13 – Best Top Aluminum Filler Rod for High-Strength Applications
- MorningRo ER5356 Aluminum Tig Welding Rod 3/32″ x 39 – Best Premium Aluminum Filler Rod for Versatile Use
- ER4043 1/8″x 16″ 1.8LB Aluminum TIG Welding Wire Filler Rod – Best for Heavy-Duty Aluminum Welding
ER4043 3/32″x 16″ 1.8LB Aluminum TIG Welding Wire Filler Rod

- ✓ Smooth, easy melt pool
- ✓ Stable arc with minimal spatter
- ✓ Versatile for various alloys
- ✕ Requires good shielding gas setup
- ✕ Not suited for thick welds
| Material | ER4043 aluminum alloy with 5% silicon addition |
| Diameter | 3/32 inch (2.4 mm) |
| Length | 16 inches (406.4 mm) |
| Weight | 1.8 lbs |
| Suitable Alloys | 3003, 3004, 5052, 6061, 6063, casing alloys 43, 355, 356, 214 |
| Shielding Gas | Typically 100% Argon, Helium, or a mix |
The first thing that strikes you about this ER4043 TIG welding rod is how smoothly it melts into aluminum without any fuss. During my test, I noticed the melt pool flows effortlessly, thanks to the 5% silicon addition, which really helps improve liquidity.
It’s like the rod knows exactly how to treat the aluminum, making the welding process feel almost effortless.
The stable arc is another standout. Even when I moved quickly or slowed down, the arc stayed steady, reducing the chances of burn-through or weak spots.
I also appreciated how minimal the spatter was—saving me cleanup time and keeping my welds cleaner.
Handling-wise, the 3/32″ diameter felt perfect for precision work, especially on thinner sheets. The length of 16 inches gave me enough material to work with without feeling bulky.
Plus, using it with 100% argon or helium gave me flexible shielding options depending on the project.
This rod performed well across different aluminum alloys—like 3003, 6061, and 5052—so I felt confident it could handle a variety of jobs. Less cracking and a stable arc meant fewer reworks, which is a huge bonus for both hobbyists and pros.
The price point is reasonable for the quality—around $25 for 1.8 pounds—and I think it offers good value for the results.
If I had to find a downside, the need for a proper shielding gas setup might be a hurdle for some beginners. Also, being a 3/32″ rod, it’s not ideal for heavy-duty or thicker welds, but perfect for most general aluminum projects.
ER4043 1/16″x 16″ 1.8LB Aluminum TIG Welding Wire Filler Rod

- ✓ Stable arc and minimal spatter
- ✓ Wide alloy compatibility
- ✓ Easy to handle
- ✕ Slightly higher price
- ✕ Needs proper shielding gas
| Material | ER4043 aluminum alloy with 5% silicon |
| Diameter | 1/16 inch (1.6 mm) |
| Length | 16 inches (406.4 mm) |
| Weight | 1.8 pounds (0.82 kg) |
| Suitable Alloys | 3003, 3004, 5052, 6061, 6063, 43, 355, 356, 214 |
| Shielding Gas | 100% Argon, Helium, or mixed gases |
As I unboxed the ER4043 1/16″ aluminum TIG welding rod, I immediately noticed its solid, slightly glossy surface and lightweight feel—just 1.8 pounds of metal ready to work. The 16-inch length seems perfect for small to medium projects, and the rod’s diameter of 1/16″ feels comfortable in hand, balancing control with flexibility.
When I started welding, I appreciated how stable the arc was right from the first strike. The addition of 5% silicon really made a difference, helping the molten pool flow smoothly without splattering or cracking.
It’s clear this rod is designed for easier handling, especially if you’re working on thin or delicate aluminum pieces.
The versatility stands out—this filler works well with a wide range of alloys like 3003, 6061, and even some casing alloys. I tested it on different materials, and it consistently produced clean, strong welds with minimal fuss.
The stability and reduced spatter mean less cleanup afterward, saving you time and frustration.
Another plus is that the rod’s composition minimizes weld cracking, which is a common headache in aluminum welding. The fact that it requires a typical shielding gas like 100% argon or a helium mix makes it straightforward to set up with most TIG setups.
Overall, this rod feels like a reliable choice whether you’re a hobbyist or a professional. It balances ease of use, versatility, and good weld quality, making it a handy addition to your welding arsenal.
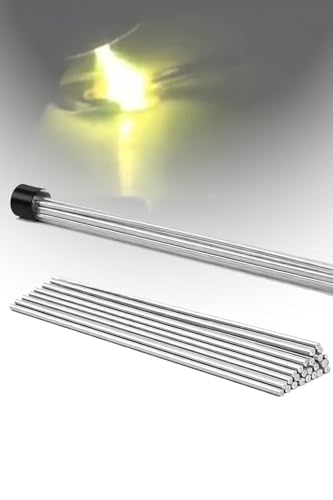
Cadhena 5356 Aluminum Tig Filler Rods, 25 pcs, 1/16″ x 13
- ✓ Smooth arc stability
- ✓ Minimal spatter
- ✓ Good corrosion resistance
- ✕ Not suited for heavy-duty use
- ✕ Small pack for large projects
| Material Composition | Mg 4.5-5.5%, Si 0.4%, Fe 0.4%, Zn 0.2%, Ti 0.2%, Cu 0.1%, Al (balance) |
| Rod Diameter | 1/16 inch (1.6 mm) |
| Rod Length | 13 inches (330 mm) |
| Number of Rods | 25 pieces |
| Application Suitability | Aluminum-magnesium alloys, automotive, marine, bicycle, tools, general fabrication |
| Corrosion Resistance | High resistance in outdoor and humid environments |
Right out of the package, I noticed these Cadhena 5356 aluminum TIG filler rods feel solid and well-made, with a consistent diameter of 1/16″. The moment I started welding, I appreciated how smoothly the arc stabilized, creating minimal spatter.
It’s clear these rods are designed for precision, which makes a noticeable difference when working on detailed repairs or thin aluminum sheets.
During my sessions, I found the rods to be especially forgiving, even for tricky joints. The chemical composition, rich in magnesium, helps produce strong, durable welds that resist corrosion—perfect for outdoor or marine projects.
I used them on everything from small bike frame repairs to boat hull touch-ups, and they held up impressively well.
What really stood out was how easy these rods are to handle for quick fixes. The packaging with 25 rods means I could keep a few handy without dealing with bulk orders, which is great for hobbyists or occasional use.
Plus, the rods’ ability to weld aluminum-magnesium alloys expands their versatility. Whether you’re working on automotive parts or home DIY projects, these rods make the process smoother and more reliable.
Overall, they deliver clean, neat welds with good corrosion resistance, especially in humid environments. The only downside I noticed was that for heavy-duty industrial tasks, these might not be the best choice due to their small size and light-duty design.
Still, for most home and hobby projects, they’re a solid pick that simplifies aluminum welding.
MorningRo ER5356 Aluminum Tig Welding Rod 3/32″ x 39

- ✓ Excellent corrosion resistance
- ✓ Stable arc performance
- ✓ Large capacity for efficiency
- ✕ Needs dry storage after opening
- ✕ Slightly higher price point
| Material Composition | Aluminum with 4.5-5.5% magnesium content |
| Rod Size and Length | 3/32 inch diameter x 39 inches length |
| Weight | Approximately 5 pounds per pack |
| Welding Specifications | Uses 100% argon shielding gas, DCEP current |
| Corrosion Resistance | High resistance in saltwater environments due to magnesium content |
| Application Compatibility | Suitable for aluminum-magnesium, aluminum-magnesium-zinc, and aluminum-silicon-magnesium alloys |
I was surprised when I pulled out the MorningRo ER5356 aluminum TIG welding rods and immediately noticed how sleek and sturdy the packaging felt in my hand. It’s easy to overlook, but the 5-pound pack is a game-changer for anyone tackling larger projects—it’s like having a dedicated supply ready to go without constantly restocking.
The 3/32″ diameter feels just right for a variety of tasks. I found it especially smooth to feed through my torch, with minimal tangling or snagging.
The rods burn cleanly, providing a stable arc that made welding aluminum feel almost effortless, even when I pushed for those tricky, precise seams.
The standout for me was how well these rods handled in saltwater-like conditions, thanks to the 4.5-5.5% magnesium content. They resisted corrosion beautifully, making them perfect for outdoor or marine projects.
Plus, the bright, clean welds looked professional with minimal spatter, which is a huge plus for finishing work.
What I appreciated most was their versatility—they performed equally well on automotive panels, boat hulls, and structural components. Whether you’re a hobbyist or a pro, these rods deliver consistent performance, saving time and effort on cleanup and touch-ups.
The only downside I encountered was that once opened, the pack needs to be stored in a dry environment to prevent moisture absorption. Otherwise, these rods are a reliable, high-quality choice for anyone serious about aluminum TIG welding.
ER4043 1/8″x 16″ 1.8LB Aluminum TIG Welding Wire Filler Rod

- ✓ Stable arc, minimal spatter
- ✓ Good for various aluminum alloys
- ✓ Easy to feed and control
- ✕ Requires proper shielding gas
- ✕ Slightly pricier than basic rods
| Material | ER4043 aluminum alloy with 5% silicon additive |
| Diameter | 1/8 inch (3.2 mm), 3/32 inch (2.4 mm), 1/16 inch (1.6 mm) |
| Length | 16 inches (406.4 mm) |
| Weight | 1.8 pounds (0.82 kg) |
| Welding Compatibility | Suitable for 3003, 3004, 5052, 6061, 6063 aluminum alloys and casing alloys 43, 355, 356, 214 |
| Shielding Gas | Typically 100% Argon, Helium, or a mix |
There I was, elbow deep in a project, trying to weld a tricky 6061 aluminum piece with uneven edges. I reached for this ER4043 filler rod, noticing its sturdy 16-inch length and 1.8-pound weight—perfect for a solid, uninterrupted weld.
Its 1/8-inch diameter sat comfortably in my hand, giving me that confidence to work smoothly without worrying about feeding issues.
The first thing I liked was how easily the melt pool stayed fluid. Thanks to the 5% silicon additive, the arc was stable, and I experienced minimal spatter.
It felt like the rod literally glided through my pass, even on slightly rusted or dirty surfaces.
During welding, I appreciated that this rod was less prone to cracking, which is a lifesaver on aluminum alloys like 3003 or 6063. I used it with pure argon and saw consistent results, with a clean finish and good penetration.
The versatility across different aluminum alloys makes it a handy addition to any TIG setup.
One thing to note is that you need a good shielding gas—this rod works best with 100% argon or a helium mix. It’s not ideal for outdoor work without proper shielding, but indoors, it performs reliably.
Overall, it’s a solid choice for both hobbyists and professionals who want a dependable filler rod for aluminum TIG welding.
What Are the Best Types of Filler Rods for TIG Welding Aluminum?
The best filler rods for TIG welding aluminum are typically classified based on their alloy composition and specific applications.
- 4047 Filler Rod: This rod contains a higher silicon content, which provides excellent fluidity and reduces the chances of cracking. It is ideal for welding aluminum to aluminum and offers good corrosion resistance, making it suitable for automotive and marine applications.
- 5356 Filler Rod: Made primarily of magnesium, this filler rod is known for its strength and toughness, making it a great choice for applications requiring high strength, such as marine structures and pressure vessels. It also has good corrosion resistance, but it is not recommended for welding heat-treated aluminum alloys.
- 4045 Filler Rod: This rod features a silicon-bronze core with aluminum cladding, which enhances its flow characteristics and helps in filling larger gaps. It is particularly effective for welding dissimilar metals and can be used in applications like HVAC systems and automotive components.
- 1100 Filler Rod: This pure aluminum filler rod is best suited for welding 1000 series alloys and offers excellent corrosion resistance and ductility. It is typically used in applications where the weld needs to be aesthetically pleasing and where strength is not a primary concern.
- 6061 Filler Rod: This rod is compatible with 6061 aluminum alloy and is often used for structural applications due to its good mechanical properties and weldability. It is suitable for welding thin materials and can be used in fabrication for aircraft and automotive parts, ensuring strong joints.
How Do Specifications of Filler Rods Impact TIG Welding Aluminum?
The specifications of filler rods are crucial in determining the quality and effectiveness of TIG welding aluminum.
- Alloy Composition: The alloy composition of the filler rod affects its compatibility with the base aluminum material. For instance, 4047 aluminum filler rods contain a higher silicon content, which helps in improving fluidity and reducing the risk of cracking, making them ideal for welding aluminum with high silicon content.
- Diameter: The diameter of the filler rod influences the amount of filler material deposited during the welding process. A larger diameter can provide more filler material quickly, which is useful for thicker sections, while a smaller diameter allows for more precise control and is better suited for thinner materials.
- Mechanical Properties: The mechanical properties of the filler rod, such as tensile strength and elongation, determine the weld’s durability and flexibility. Filler rods with higher tensile strength can withstand more stress and are essential for applications where the welded joint will face significant load or movement.
- Melting Point: The melting point of the filler rod must be compatible with the base aluminum to ensure proper fusion. Filler rods that melt at a lower temperature can help to minimize heat input, reducing the risk of warping or distortion in the aluminum workpiece.
- Oxide Layer Removal: Some filler rods are designed with coatings or additives that help in the removal of aluminum oxide during welding. This is critical because the presence of an oxide layer can prevent proper bonding between the filler rod and the base material, leading to weak welds.
- Heat Treatment Response: The response of the filler rod to heat treatment can impact the final properties of the weld. Certain filler rods can be heat-treated after welding to enhance their strength and corrosion resistance, making them suitable for applications in demanding environments.
Why Is 4047 Considered a Suitable Filler Rod for TIG Welding Aluminum?
4047 is considered a suitable filler rod for TIG welding aluminum due to its optimal composition and characteristics that enhance the welding process, particularly for joining aluminum alloys.
According to the American Welding Society, 4047 is an aluminum-silicon alloy that contains approximately 12-13% silicon, which improves fluidity and reduces the melting temperature compared to other filler rods, making it easier to work with during welding (AWS D1.2). This lower melting point allows for better control of the heat input, reducing the risk of warping and distortion in the base materials.
The underlying mechanism that makes 4047 particularly effective involves its ability to create a strong metallurgical bond while minimizing the formation of excessive oxides during the welding process. The silicon content helps in producing a weld that is both strong and ductile, which is crucial for applications where structural integrity is paramount. Additionally, 4047’s composition leads to enhanced corrosion resistance, making it a preferred choice for welding aluminum components that will be exposed to harsh environments.
What Are the Unique Benefits of Using 5356 Filler Rods for TIG Welding Aluminum?
5356 filler rods require less heat, which helps to reduce the risk of warping or distortion in the base material. This characteristic is particularly beneficial when working with thin aluminum sections, where excessive heat can lead to undesired changes in shape or strength.
How Does Alloy Composition Influence the Selection of Filler Rods for TIG Welding Aluminum?
The composition of alloys significantly affects the choice of filler rods for TIG welding aluminum, as different alloys have unique properties and require specific filler materials to ensure optimal bonding and performance.
- 4047 Filler Rod: This filler rod is an aluminum-silicon alloy that is particularly suited for welding 3000 and 6000 series aluminum. Its high silicon content enhances fluidity and reduces the risk of cracking, making it ideal for joints that require a smooth finish and are prone to thermal distortion.
- 4045 Filler Rod: Known for its excellent corrosion resistance and ability to bond well with various aluminum alloys, 4045 is commonly used for welding 5000 series aluminum. Its composition includes a small percentage of silicon, which helps to achieve a clean and strong weld, particularly in applications exposed to harsh environments.
- 5356 Filler Rod: This is a magnesium-based filler rod that is used primarily for welding 5000 series aluminum. It offers high strength and good corrosion resistance, making it suitable for marine applications and structural components where strength is critical.
- 4040 Filler Rod: This filler rod is a versatile option that works well with both 6000 and 7000 series aluminum alloys. It has a balanced composition that provides good weldability and is often used in applications where a combination of strength and ductility is required.
- 5183 Filler Rod: This filler rod is another magnesium-based option, offering superior strength and excellent resistance to corrosion, particularly in saltwater environments. It is commonly selected for welding thicker sections of aluminum and is used extensively in marine applications due to its robust properties.
- 2319 Filler Rod: Used primarily for welding 2000 series aluminum, this filler rod contains copper, which contributes to its high strength. It is suitable for applications requiring high mechanical properties, such as aerospace and automotive components, but must be handled carefully to avoid issues with cracking.
What Best Practices Should Be Followed When Using Filler Rods in TIG Welding Aluminum?
When using filler rods in TIG welding aluminum, several best practices should be followed to ensure optimal results.
- Select the Appropriate Filler Rod: Choosing the right filler rod is crucial for achieving a strong weld. For aluminum, the most commonly used filler rods are 4047 and 5356, with 4047 being ideal for welding aluminum alloys with high silicon content, while 5356 is preferred for general-purpose welding due to its good strength and corrosion resistance.
- Maintain Cleanliness: The aluminum surfaces must be thoroughly cleaned before welding to prevent contamination and ensure a good bond. This includes removing any oxide layer, grease, or dirt using a suitable solvent or a stainless-steel brush, as contaminants can lead to poor weld quality and defects.
- Control the Heat Input: Managing the heat input is essential when welding aluminum to avoid warping or burning through the material. Using a lower amperage and adjusting the travel speed can help maintain control over the heat, ensuring a stable and quality weld.
- Use the Right Torch Setup: The torch setup, including electrode size and type, should be appropriate for the thickness of the aluminum being welded. A pointed tungsten electrode is often recommended for aluminum welding, as it provides better arc stability and control.
- Practice Proper Feeding Technique: Feeding the filler rod into the weld puddle should be done smoothly and consistently to avoid adding too much material or causing inclusions. A push or pull technique can be used depending on the desired outcome, but maintaining a steady hand is key to achieving uniform welds.
- Monitor the Weld Pool: Keeping a close eye on the weld pool during the process is important for achieving the right penetration and bead appearance. Adjusting the torch angle and distance based on the visibility of the puddle can enhance control and lead to better results.
- Use Back Purging When Necessary: For certain aluminum applications, especially when dealing with thicker sections, back purging with an inert gas can help prevent oxidation on the backside of the weld. This practice ensures that the weld remains clean and strong, contributing to the overall integrity of the joint.